High-Speed Rotary Compression
Multi-station rotary presses capable of producing bi-layer, chewable, sublingual, time-release, and effervescent tablets. Includes full film, color, and pharmaceutical glaze coating capabilities.
At Bactolac Pharmaceutical, we believe in 100% operational transparency for our international partners and brand owners. Located in Hauppauge, New York, our state-of-the-art 650,000 square foot manufacturing plant is designed specifically for large-scale, turn-key dietary supplement production.
Our facility operates under strict U.S. FDA 21 CFR Part 111 cGMP guidelines and is independently registered by NSF. Equipped with advanced climate-control and industrial HVAC systems, every suite maintains regulated ambient humidity and positive air pressure to safeguard raw ingredients and maintain microbial purity throughout production.
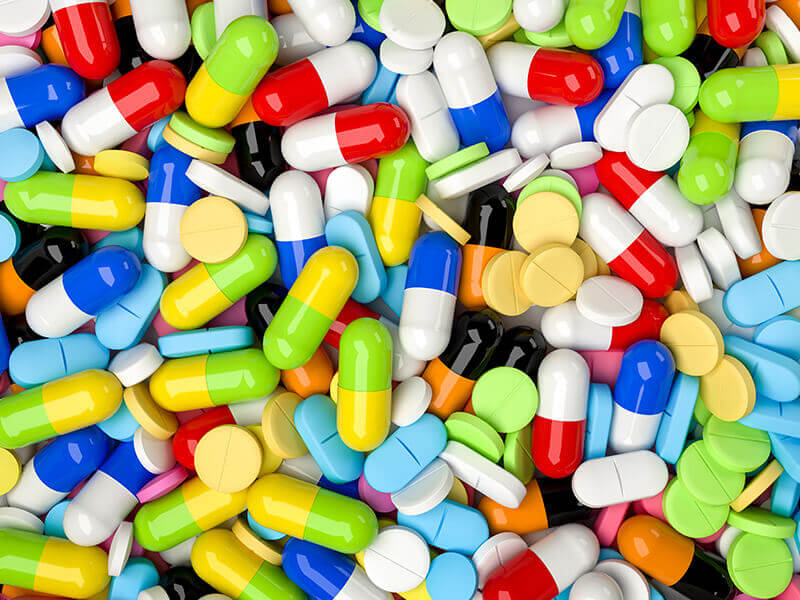
Engineered for high-volume execution, our production floors are equipped with pharmaceutical-grade machinery to ensure precise batch consistency and fast turnarounds for global market distribution.
Multi-station rotary presses capable of producing bi-layer, chewable, sublingual, time-release, and effervescent tablets. Includes full film, color, and pharmaceutical glaze coating capabilities.
Fully automatic high-speed encapsulation machines processing size 000 to 4 two-piece vegetarian and gelatin capsules, liquid-filled hard veggie capsules, and delayed-release formulations.
FDA-compliant V-blenders and ribbon blenders handling bulk protein powders, greens, electrolytes, and complex botanical formulations with uniform particle dispersion.
Equipped with HPLC, GC-MS, and micro-testing apparatus for incoming raw material identity verification, heavy metals, pesticides, and finished lot Certificate of Analysis (CoA) release.
High-speed bottling, blister packaging, stick packs, single-serve sachets, gusset bags, and shrink-wrapping lines with automated vision systems for label application.
Dust-contained material transport, automated gravity distribution silos, and climate-controlled raw material quarantine warehousing ensuring supply chain traceability.
Global procurement teams demand manufacturing partners with scalable capacity, predictable lead times, and robust quality management systems. Our plant infrastructure is optimized to remove supply bottlenecks:
Examine our production bays, automated packaging automation, and analytical testing labs from anywhere in the world.
Essential information for overseas sourcing managers and brand owners evaluating our facility for contract manufacturing partnerships.
Our primary manufacturing plant in Hauppauge, New York spans 650,000 sq. ft. It is fully cGMP-compliant and equipped with industrial climate control, relative humidity management, and HEPA air filtration suites to guarantee ingredient stability and cleanroom safety.
Yes. We welcome third-party auditor inspections and on-site buyer visits. For overseas procurement teams unable to travel, our compliance team hosts live video audits and provides full Master Batch Records, SOP documentation, and facility layouts.
Our facility houses dedicated microbiological and analytical chemical laboratories. Equipment includes HPLC, GC-MS, ICP-MS (heavy metal testing), FTIR spectrophotometers, and dissolution apparatus for end-to-end quality assurance.
Production occurs in dust-contained, isolated processing suites with individual HVAC air handlers. Equipment undergoes validated multi-stage cleaning procedures and micro-swab testing between batch runs to eliminate allergen cross-contact.
Contact our technical team to schedule a plant audit, request product catalogs, or receive a fast contract manufacturing quote.