Explore our benchmark private label and OEM/ODM product formats engineered for global brand scaling and rigorous regulatory compliance in the Australian and Asia-Pacific markets.
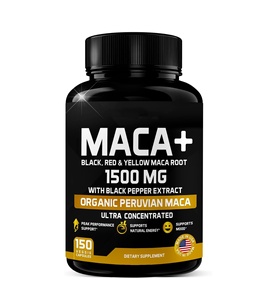
High-potency adaptogenic herbal complex featuring dual Red & Yellow Maca botanical extracts for endocrine balance, stamina, and vital energy delivery.
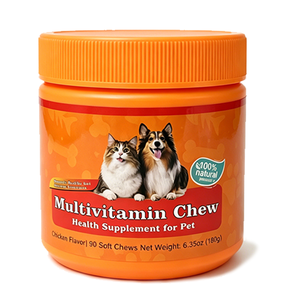
Advanced veterinary-grade microencapsulated probiotic strain blend combined with digestive enzymes in dual-layer chewable tablet format.
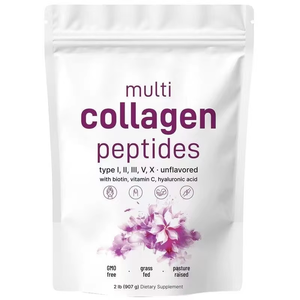
Hydrolyzed Type I & III collagen peptides fortified with buffered Vitamin C for enhanced bioavailability, structural bone density, and skin elasticity.
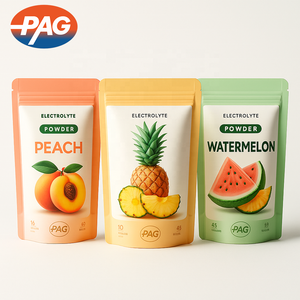
Rapid-osmolality cellular hydration matrix utilizing bio-identical sodium, potassium, and magnesium ratios for high-endurance athletic performance.
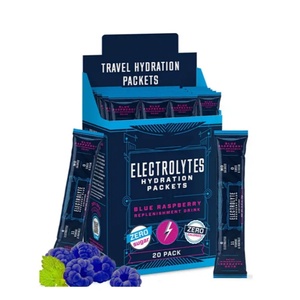
Dual-action metabolic energizer pairing sustained-release B-complex vitamins with essential trace mineral electrolytes in portable single-serve sachets.
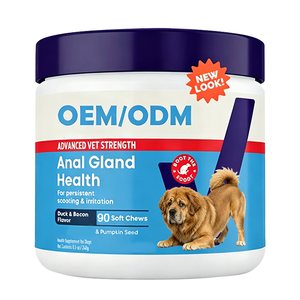
High-fiber dietary chew containing proprietary pumpkin seed, beet pulp, and active probiotic cultures formulated specifically for companion animal GI stability.
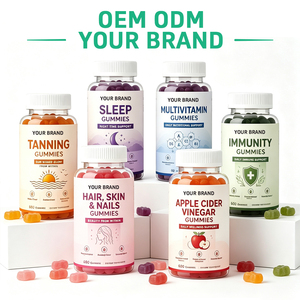
Pectin-based, non-GMO gummy delivery platform engineered with thermal stability controls to preserve sensitive active botanical compounds and vitamins.
Naturally sweetened clean-label electrolyte mix engineered for quick gastric emptying and rapid fluid absorption without synthetic dyes or additives.
The health and wellness sector across Victoria, Australia—and specifically within the vibrant Melbourne retail and clinical healthcare landscape—is undergoing a profound technological transformation. Consumers are demanding sophisticated, clean-label, multi-functional nutraceutical solutions that deliver measurable physiological outcomes. Traditional single-layer compression tablets are frequently inadequate when formulating modern, complex nutritional regimens requiring immediate-release (IR) combined with extended-release (ER) kinetics, or when combining physically or chemically incompatible active pharmaceutical and nutraceutical ingredients (APIs).
Bi-layer tableting technology addresses these fundamental formulation challenges by compressing two distinct granulated matrices into a single, cohesive solid dose format. This dual-layer architecture prevents chemical cross-reactivity (such as direct contact oxidation between ascorbic acid and sensitive trace minerals) while optimizing the pharmacokinetic absorption window across the gastrointestinal tract.
Key Insight for Sourcing Directors: Bi-layer tableting eliminates consumer pill fatigue in the Australian market by consolidating morning and evening dosing regimens into a single, once-daily dual-stage tablet.
Evaluating contract manufacturing partners requires strict scrutiny of engineering precision, analytical quality units, and regulatory compliance frameworks. Sourcing executives use the following 10 core benchmarks to audit high-capacity bi-layer factories.
High-speed rotary tablet presses equipped with independent weight monitoring, pre-compression tamping stations, and real-time displacement sensors to prevent layer separation (delamination).
Proven physical separation protocols for ingredients susceptible to chemical degradation upon physical contact, ensuring maximum shelf-life potency over 24 to 36 months.
Full compliance with U.S. FDA dietary supplement cGMP guidelines, structured to seamlessly integrate with Australian Therapeutic Goods Administration (TGA) import specifications.
Engineered dissolution profiling enabling Layer 1 to disintegrate within 15 minutes in gastric fluids while Layer 2 undergoes zero-order or first-order sustained release over 8–12 hours.
On-site laboratories utilizing HPLC, FTIR, ICP-MS, and automated micro-biology screening to verify active potencies, heavy metals, and pathogen limits on every batch.
Scientific determination of optimum compaction pressure ratios (kN) to achieve exceptional hardness while preserving layer boundaries without structural shear failure.
Distinctive chromatic contrast between layers using natural, clean-label botanical colorants (e.g., spirulina blue, beet powder red) for powerful shelf appeal and consumer brand recognition.
Aqueous or organic protective film coatings engineered to shield sensitive active ingredients from Australia’s variable humidity and temperature transport conditions.
Master Batch Records (MBR), Certificates of Analysis (COA), Allergen declarations, non-GMO verifications, and BSE/TSE statements required for smooth customs release.
End-to-end management spanning raw material procurement, formulation science, tablet compression, laboratory release, and final retail packaging in bottles or blister packs.
Manufacturing bi-layer tablets is vastly more complex than standard compression. It requires precise control of compaction kinetics, dwell time, and granular properties.
The primary failure mode in bi-layer tableting is delamination—the structural separation of Layer 1 from Layer 2 during ejection or handling. Preventing delamination depends on managing the ratio between initial tamping force (Pre-compression) and final main compression force.
During the first stage, Layer 1 receives a light tamping force (typically 1 to 5 kN). This creates sufficient pore space and surface roughness for Layer 2 granules to interlock when main compression (15 to 35 kN) is applied. Over-compacting Layer 1 eliminates micro-voids, preventing mechanical interlocking and leading to interfacial fracture.
Matching the plastic deformation profiles of both layers is critical. If Layer 1 exhibits high elastic recovery while Layer 2 undergoes plastic deformation, the differential stress relaxation post-compression causes shearing at the layer boundary. Our formulation scientists optimize excipients—selecting microcrystalline cellulose (MCC), dicalcium phosphate, and tailored disintegrants—to harmonize elastic recovery curves across both layers.
Understanding how Victoria’s health-conscious consumers utilize dietary supplements enables brand owners to bring differentiated products to market faster.
Scenario: Executive professionals in Melbourne's financial and tech sectors require daytime cognitive focus followed by restorative evening sleep.
Bi-Layer Solution: Layer 1 delivers fast-acting L-Theanine and quick-release herbal adaptogens, while Layer 2 slowly releases botanical extracts and magnesium over 8 hours to support deep sleep cycles.
Scenario: Athletes participating in Melbourne's marathon and endurance culture need immediate hydration and long-lasting muscular stamina.
Bi-Layer Solution: Layer 1 offers rapid-dissolving electrolytes (Sodium/Potassium), while Layer 2 slow-releases B-complex vitamins and CoQ10 to maintain mitochondrial ATP synthesis without energy crashes.
Scenario: Gut health supplements designed for Melbourne's booming wellness market requiring live probiotic strains alongside concentrated plant actives.
Bi-Layer Solution: Layer 1 isolates delicate probiotic strains from moisture, while Layer 2 houses acidic or reactive botanical extracts like Cranberry or Garlic extract.
Scenario: An aging demographic seeking once-daily joint discomfort relief and long-term cartilage support.
Bi-Layer Solution: Layer 1 provides immediate analgesia support with fast-acting Boswellia serrata, while Layer 2 delivers slow-release Glucosamine and Chondroitin matrix over 12 hours.
Scenario: Clean-label daily multivitamins where sensitive vitamins (like C and B12) degrade rapidly in the presence of trace minerals (Iron and Copper).
Bi-Layer Solution: Complete physical separation into two distinct color-coded layers, stabilizing active potency throughout shelf life without requiring artificial chemical coatings.
Scenario: Australian pet owners seeking palatable, high-efficacy digestive and joint support chews for dogs.
Bi-Layer Solution: Layer 1 features a savory meat-flavored chewable base with digestive enzymes, while Layer 2 houses concentrated Omega fatty acids and probiotic cultures.
Since 1995, Bactolac Pharmaceutical has provided full-service turn-key contract manufacturing for leading global dietary supplement brands from our state-of-the-art facilities in New York, USA.
Everything that dictates product success—formulation science, raw material quarantine, precision blending, bi-layer tableting, analytical testing, and final labeling—takes place under a single unified quality system.
Raw materials are quarantined and identity-verified upon arrival. Finished bi-layer lots undergo potency, heavy metal, disintegration, and microbiological testing in our on-site laboratories prior to release.
We formulate without unnecessary binders or artificial fillers. Our flavor technologists specialize in masking bitter botanicals, amino acids, and minerals so your bi-layer products deliver outstanding taste.
From high-density polyethylene (HDPE) bottles and glass jars to blister packs and display cartons, we deliver fully labeled, retail-ready inventory direct to your Melbourne distribution center.
Our operations strictly adhere to FDA 21 CFR Part 111 cGMP regulations and hold prestigious third-party audits and certifications:
Compare structural engineering characteristics, release capabilities, and formulation stability parameters across common solid oral dosage formats.
| Delivery Format | Release Kinetics Profile | Active Ingredient Separation | Physical Stability & Moisture Control | Production Complexity |
|---|---|---|---|---|
| Bi-Layer Tablets | Dual-Phase (Immediate + Extended Release) | Excellent (Physical Layer Barrier) | High (Engineered Film & Core Barrier) | High (Rotary Dual-Compression) |
| Single-Layer Tablets | Single-Phase (Immediate Release only) | Poor (Direct Contact Mix) | Moderate (Depends on Coating) | Standard (Single Compression) |
| Hard Capsules (Two-Piece) | Standard Fast-Dissolve | Fair (Powder Premix) | Moderate (HPMC/Gelatin Sheath) | Moderate (Encapsulation Fill) |
| Softgels | Rapid Liquid Dissolution | Poor (Homogeneous Liquid Suspensions) | Low (Sensitive to Heat & Humidity) | High (Rotary Die Process) |
| Effervescent Tablets | Instant Aqueous Solution | Poor (Immediate Organic Acid Reaction) | Low (Requires Strict Desiccant Packaging) | High (Humidity-Controlled Suite) |
Key insights regarding customs compliance, batch scalabilities, bi-layer technology troubleshooting, and international export protocols.
Our US-based facilities operate under FDA 21 CFR Part 111 cGMP regulations. Products imported into Australia as complementary medicines or dietary supplements are evaluated against TGA standards. We provide complete documentation packages—including Certificates of Analysis (COA), Master Batch Records, allergen statements, and BSE/TSE declarations—to facilitate smooth clearance through Australian Border Force and customs compliance audits.
Delamination is controlled during formulation development by selecting excipients with compatible plastic deformation dynamics. During production, our rotary presses utilize precise pre-compression tamping forces (1–5 kN) to lightly consolidate Layer 1, leaving surface roughness for mechanical interlocking when Layer 2 undergoes main compression (15–35 kN). Every lot undergoes friability and hardness stress testing to ensure structural integrity across global shipping routes.
Yes. We specialize in natural, clean-label coloring systems utilizing spirulina extract, beet root powder, turmeric, and riboflavin. Providing sharp visual contrast between layers enhances shelf visibility and reinforces dual-action consumer claims without resorting to synthetic FD&C dyes.
Production timelines depend on raw material availability, custom tooling requirements, and analytical release testing. Typical initial orders range from pilot batches to large commercial runs. Repeat orders move significantly faster once raw material supply chains and analytical methods are locked with your dedicated project manager.
Every production batch undergoes comprehensive testing in our on-site laboratories: active potency assay (HPLC/UV), heavy metal screening (ICP-MS), disintegration and dissolution profiling across both layers, tablet weight variation, thickness, friability, and micro-biology limits (Total Plate Count, Yeast/Mold, E. coli, Salmonella).
Absolutely. We provide turn-key packaging solutions including HDPE and PET bottles, wide-mouth glass jars, blister packs, outer cartons, tamper-evident neck bands, and induction seals. Full label application and batch coding are completed in-house so your goods arrive retail-ready for immediate Australian distribution.
Partner with an established 30-year turn-key manufacturer. Contact our formulation team today to review your bi-layer tablet specification, request sample batches, and access our complete master catalog.