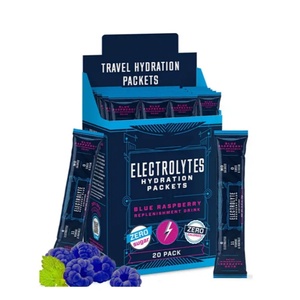
Explore our flagship OEM/ODM dietary supplement portfolio—engineered, blended, encapsulated, and packaged in our US-based cGMP facilities for brands in Boston, regional distributors, and global exporters.
Providing Greater Boston, New England enterprise brands, and international importers with science-backed electrolyte formulations, high-shear powder blending, and compliant stick-pack packaging.
Technical Information Gain Note: Unlike re-packers or brokers, our contract manufacturing operational hub operates directly under US FDA 21 CFR Part 111 cGMP regulations. From our strategic East Coast location near Boston supply lines, we manage raw material quarantine, particle mesh verification, osmolality balancing, and shelf-stable packaging in-house.
Electrolyte efficiency depends on cellular bio-availability and osmolality balance. Our formulation scientists craft custom ionic ratios utilizing Albion chelated magnesium, sodium chloride, potassium citrate, calcium glycerophosphate, and trace minerals.
Hygroscopic electrolyte minerals require strict relative humidity (RH) ambient controls to prevent clumping. Our high-capacity ribbon blenders ensure micro-ingredient homogenization down to parts-per-million accuracy across multi-ton production batches.
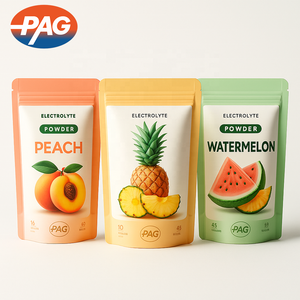
We supply turnkey retail packaging solutions designed for modern consumer convenience. From narrow single-serve stick packs designed for water bottles to multi-serve wide-mouth HDPE tubs, our packaging lines operate with strict seal-integrity testing.
The Greater Boston area represents a unique convergence of elite endurance sports, world-leading academic & life science research, micro-climate weather volatility, and demanding maritime industries.
Boston is home to world-renowned athletic traditions, including the Boston Marathon, collegiate rowing along the Charles River, and NCAA athletic programs. Local brands catering to high-performance athletes require specialized hypotonic electrolyte mixes that facilitate ultra-rapid gastric emptying and cellular hydration during long-distance training runs in humid New England summers.
In the innovation hubs of Kendall Square, Cambridge, and the Longwood Medical Area, life science startups and medical technology companies are pioneering clinical-grade oral rehydration solutions (ORS). Our cGMP manufacturing facility supports clinical trial batch runs and medical-grade electrolyte blends engineered strictly according to WHO (World Health Organization) osmolarity guidelines.
From dockworkers at the Port of Boston to commercial cold-storage technicians and heavy infrastructure crews operating along I-90 / I-95, severe thermal stress (both extreme winter dry-air dehydration and summer heat stress) is a critical occupational hazard. We manufacture zero-sugar, high-sodium industrial electrolyte replenishment packets for regional workplace safety suppliers.
Analyzing consumer shifting behaviors, functional ingredients demand, and formulation metrics across New England retail networks.
Boston consumers lead national trends in scrutinizing supplement facts panels. There is an explosive demand for zero-artificial-color formulations, stevia/monk fruit sweetener systems, non-GMO verifications, and organic coconut water bases.
Modern consumers expect dual-benefit functional drink mixes. Formulations integrating electrolytes with L-Theanine, Alpha-GPC, Organic Ashwagandha, and Rhodiola Rosea are capturing premium market share among Boston’s tech and academic professionals.
Traditional 500g tubs are yielding market share to portable stick packs (7g - 10g single-serve sachets). Modern consumers favor convenience, precise dosage, and water-bottle-friendly pour spouts.
| Formulation Profile | Target Sodium / Potassium Ratio | Osmolality (mOsm/kg) | Ideal Application Scenario | Key Active Ingredients |
|---|---|---|---|---|
| Hypotonic Rapid-Hydration | 3 : 1 Ratio (High Sodium) | 200 - 240 mOsm/kg | Marathon Endurance & Extreme Heat | Pink Himalayan Salt, Potassium Citrate, Magnesium Glycinate |
| Isotonic Daily Balance | 2 : 1 Ratio (Balanced) | 270 - 330 mOsm/kg | Daily Wellness, Office Focus & Travel | Coconut Water Powder, Sea Salt, Calcium Lactate, Trace Minerals |
| Nootropic Focus Hydration | 1.5 : 1 Ratio | 250 - 290 mOsm/kg | Academic, Tech & Executive Performance | Electrolytes, L-Theanine, Cognizin® Citicoline, Vitamin B-Complex |
| WHO-Standard Clinical ORS | 1 : 1 Glucose-Sodium Co-transport | 245 mOsm/kg | Medical Grade, Travel & Severe Recovery | Dextrose, Sodium Chloride, Potassium Chloride, Trisodium Citrate |
Over three decades of contract supplement manufacturing expertise backed by rigorous analytical science, scalable capacity, and total turn-key ownership.
Founded in 1995, our manufacturing operations have built a legacy of trust with major health product retailers, direct-to-consumer digital brands, and international pharmaceutical exporters. We hold strict adherence to FDA 21 CFR Part 111 cGMP standards.
Eliminate 3rd-party testing bottlenecks. Our fully equipped on-site analytical and microbiological laboratories perform raw material identification (FTIR, HPLC), heavy metal testing (ICP-MS), and finished lot microbial screening for immediate Release Certificates (COA).
Our main manufacturing campus in Hauppauge, New York, offers optimized regional logistics directly serving the Boston metro area, Massachusetts distribution corridors, and major Northeast shipping ports, drastically reducing freight transit times and costs.
Addressing core technical, regulatory, and logistics queries for supplement brand owners, purchasing directors, and product managers.
Our MOQs are structured to accommodate growing brand startups as well as established corporate enterprise runs. For single-serve stick packs, standard custom formulation runs typically start at 50,000 to 100,000 stick packs per flavor. For multi-serve powder tubs (e.g., 30-serving jars), MOQs generally start at 1,500 to 3,000 units depending on raw material customization and flavor systems.
Electrolyte active ingredients—such as potassium chloride, magnesium citrate, and sodium chloride—are highly hygroscopic and naturally attract atmospheric moisture, causing caking. Our cleanrooms and powder blending suites feature automated HVAC relative humidity (RH) control systems maintained below 35% RH. Additionally, we utilize specialized micro-encapsulation techniques and high-barrier foil laminates to lock out ambient moisture throughout product shelf-life.
Yes. Our in-house flavor chemistry staff specializes in custom flavor matching and masking techniques. We convert naturally tart or metallic mineral bases into refreshing profiles such as Lemon-Lime, Passionfruit Mango, Blue Raspberry, and Watermelon. We work exclusively with non-artificial colors, natural fruit powders, and zero-calorie sweeteners including Stevia (Reb-M) and Monk Fruit extract.
Every single batch produced at our facility undergoes rigorous analytical testing before release. Export documentation packages include a complete Certificate of Analysis (COA) detailing physical specs, active ingredient assay values, heavy metals, micro testing, Certificate of Free Sale (CFS), cGMP compliance certificates, Allergen statements, and BSE/TSE-free declarations required by international customs authorities.
Once your custom formulation, flavor profile, and packaging design are locked, typical turn-around time for initial order execution ranges between 6 to 8 weeks, depending on raw material sourcing lead times. Repeat production runs are streamlined through strategic raw material safety stock programs, frequently reducing lead times to 4 weeks for regional Boston deliveries.