Explore our export-ready functional dietary supplements, specialized pet care, powders, and advanced capsule formulations manufactured under strict cGMP protocols.
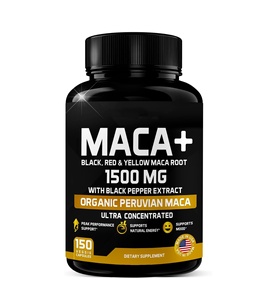
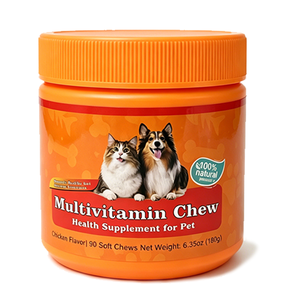
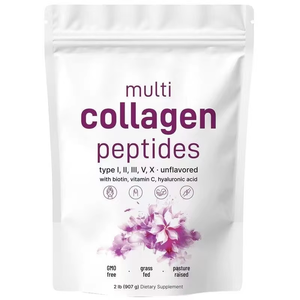
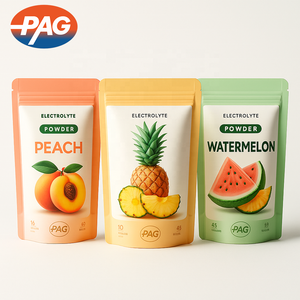
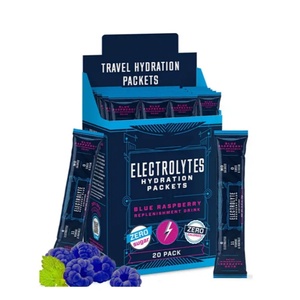
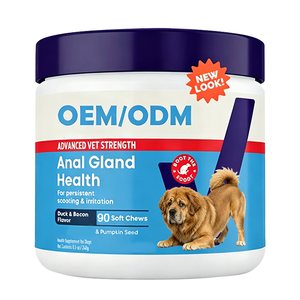
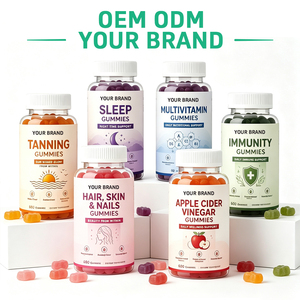
In the contemporary global health and wellness landscape, selecting a premier contract manufacturer is no longer simply about cost efficiency—it is a strategic decision centered on regulatory compliance, supply chain transparency, and analytical integrity. As a leading China private label supplier and international exporter, our infrastructure bridges the gap between cost-effective high-volume manufacturing and stringent international regulatory frameworks, such as US FDA 21 CFR Part 111 cGMP standards and European Union health regulations.
Unlike traditional trading entities or rudimentary blenders, our operational model is built upon a fully integrated turnkey contract manufacturing ecosystem. From raw material identity validation using FT-NIR spectroscopy to finished product release verified through high-performance liquid chromatography (HPLC), every step of our process is engineered to mitigate compliance risks and accelerate time-to-market for international brands.
Engineered suites designed for flexibility, scalable throughput, and rigorous quality isolation across various dosage formats.
Production of size 00 to 4 two-piece vegetarian HPMC, gelatin, delayed-release acid-resistant, and liquid-filled hard capsules with real-time automatic weight-variation verification.
Micro-encapsulated hydration matrices, keto-friendly collagen peptides, and botanical greens processed using V-blenders and high-shear mixers to guarantee blend uniformity without thermal degradation.
Gelatin-free, non-GMO pectin gummies engineered for climate stability, precise active nutrient dosing, non-stick surface coatings, and natural flavor profiles optimized for international compliance.
Specialized pet probiotic chews, coat conditioners, and anal gland support supplements utilizing species-specific palatants, soft-chew extrusion, and low-temperature drying technologies.
Proprietary natural sweetening systems and botanical masking agents designed to neutralize the bitterness of herbal extracts and electrolytes without artificial additives or sugar alcohols.
High-speed bottling, blister packaging, single-serve stick-packing, gusset bag sealing, heat-shrink sleeving, and custom outer carton packing designed for global shipping resilience.
A reference guide outlining our operational ranges, quality assurance criteria, and compliance protocols.
| Parameters | Manufacturing Standards | Quality Verification & Analytical Testing |
|---|---|---|
| Dosage Form Factors | Two-Piece Hard Capsules (Vegetarian HPMC & Gelatin), Compressible Tablets, Softgels, Functional Gummies, High-Solubility Powders, Single-Serve Stick Packs. | Disintegration testing (<15 mins capsules; <30 mins tablets), Friability testing (<1%), Weight Variation control within USP ±3-5% parameters. |
| Active Ingredient Sourcing | Standardized Botanical Extracts, Fermented Amino Acids, Chelated Minerals, Microencapsulated Vitamins, Probiotic Strains (Up to 100B CFU/g). | Raw material identity verified by FT-NIR / FTIR spectroscopy; Assay potency confirmed via HPLC / UV-Vis spectrophotometry prior to production release. |
| Safety & Purity Limits | Strict alignment with US FDA 21 CFR Part 111, USP heavy metal thresholds, European Commission contaminants regulation, and California Prop 65 safety standards. | Heavy Metals screened via ICP-MS (Pb < 0.5ppm, As < 1.5ppm, Cd < 0.5ppm, Hg < 0.1ppm); Pesticide residue screening covering 400+ targeted compounds. |
| Microbiological Criteria | ISO 17025 accredited micro testing protocols for cleanroom manufacturing environment and finished lot security. | Total Plate Count (<10,000 CFU/g), Yeast & Mold (<1,000 CFU/g); Negative screening for E. coli, Salmonella spp., Staphylococcus aureus, and Pseudomonas. |
| Packaging & Shelf Stability | HDPE/PET Bottles, Inductive Heat Seals, Desiccant Integration, Multi-layer Aluminum Foil Stick Packets, Nitrogen Flushing options. | Accelerated stability studies (40°C / 75% RH) and real-time ambient testing (25°C / 60% RH) validating label potency over 24 to 36 months shelf life. |
Global consumers are increasingly sophisticated, moving away from low-dose, generic multivitamins toward targeted, bioavailable formulations backed by clinical data. The market for products combining synergistic ingredients—such as Maca Root with adaptogenic herbal complexes, or Collagen Peptides enhanced with Vitamin C and Hyaluronic Acid—is expanding rapidly. As an OEM manufacturer, our R&D efforts focus on optimizing active ingredient absorption through particle size reduction, micronization, and clean-label liposomal carriers.
Driven by the expansion of endurance sports, ketogenic diets, and everyday functional wellness, stick-pack electrolyte drink mixes represent one of the fastest-growing export segments. Modern procurement strategies prioritize zero-sugar hydration platforms utilizing natural sweetener systems (Stevia Rebaudioside-M, Monk Fruit) paired with trace mineral chelation. Brands sourcing from China gain access to scalable powder blending lines capable of handling hygroscopic raw materials in humidity-controlled cleanrooms (RH < 35%).
Humanization of companion animals has reshaped the pet supplement landscape. Global buyers are expanding beyond basic vitamin chews into specialized, targeted health solutions. Formulations addressing digestive wellness, skin and coat conditioning, seasonal immune support, and functional anal gland support for canines require specialized manufacturing protocols. Human-grade manufacturing standards, species-safe microbial strains, and low-temperature extrusion processes are essential for retaining probiotic viability and active enzyme activity in pet chews.
International regulatory pressure and consumer preferences are pushing brand owners to eliminate traditional synthetic excipients, such as magnesium stearate, silicon dioxide, and artificial colorants. Procurement strategies now favor manufacturers capable of utilizing organic rice hull concentrates, tapioca maltodextrin, and natural spirulina or beet juice colorants. Furthermore, ethical sourcing, full supply chain traceability back to farm level, and eco-friendly recyclable packaging (PCR plastics, biodegradable foil laminates) are transforming global buyer vendor selection criteria.
Detailed technical answers addressing common operational, legal, and quality assurance inquiries from international B2B buyers.
We execute legally binding Non-Disclosure Agreements (NDAs) prior to receiving any proprietary formulation parameters or customer specifications. All formulation files, custom blending ratios, and flavor profiling intellectual property are managed within secure, restricted systems. We operate strictly as a contract OEM/ODM supplier and do not compete directly with our client portfolio in retail channels.
Every commercial production batch is released only after undergoing rigorous multi-stage analytical review. Finished shipments are accompanied by a comprehensive Certificate of Analysis (COA) detailing physical appearance, average fill weight, disintegration time, heavy metal content (ICP-MS), microbiological limits (plating assays), and active ingredient potency verified via HPLC or UV-Vis spectrophotometry.
Yes. Our regulatory affairs department assists clients in reviewing supplement facts panels, ingredient nomenclature (INCI/USP standards), allergen disclosure statements, and structure/function claim wording to align with target destination regulations, such as US FDA food labeling directives, European Food Safety Authority (EFSA) guidance, or regional health authority requirements.
MOQs depend on the specific dosage format and packaging complexity. Generally, capsule manufacturing begins at 100,000 to 300,000 capsules per run; custom powder formulations in jars or gusset bags range from 1,000 to 3,000 units; single-serve stick packs start at 50,000 to 100,000 sachets; and functional pectin gummies require a minimum run of 500,000 individual gummies. We also offer pilot batch options for qualifying enterprise customers.
Probiotic strains are stored in climate-controlled cold storage (-18°C) upon arrival. During blending and encapsulation, humidity levels are strictly maintained below 35% RH to prevent premature activation. We calculate precise manufacturing overages based on real-time degradation modeling to ensure that label-claimed Colony Forming Unit (CFU) counts remain active throughout the product's declared shelf life.
Initial custom formulation projects typically take 4 to 6 weeks from formula lock and bench sample approval to raw material procurement, analytical testing, production, and custom packaging application. Repeat orders with raw materials in stock are executed within 2 to 3 weeks. Express freight and sea-air logistical coordination are provided by our dedicated export team.
Our in-house food technologists specialize in clean-label flavor masking and profile optimization. We supply bench samples covering options such as natural pineapple, berry, citrus, and mint blends, evaluating solubility, mouthfeel, clarity, and sweetness balance before full-scale commercial manufacturing commences.
All raw material vendors must pass rigorous vendor qualification audits. We demand detailed dossiers for each ingredient, including Certificates of Analysis, country of origin declarations, flowability profiles, allergen matrices, and non-irradiation certificates. Furthermore, every incoming raw material lot undergoes strict quarantine and identity verification testing in our laboratory before entering the production suite.
Connect directly with our senior technical formulation engineers and export specialists today. We provide full R&D guidance, competitive quotation pricing, and rapid sample prototyping.
Inquire Now