Evaluating commercial-grade formulations requires assessing assay potency, ingredient matrix stability, and consumer sensory feedback. Below is a curated catalog of benchmarked dietary supplements engineered for turnkey private-label expansion and global wholesale distribution.
In an increasingly scrutinized global marketplace, selecting a multivitamin manufacturer demands rigorous technical evaluation. Search engines and regulatory bodies like the U.S. FDA enforce high transparency metrics. Sourcing directors must look beyond price-per-unit and scrutinize raw material origin, batch-to-batch analytical assays, and cGMP infrastructure.
Information Gain Insight: Over 64% of batch recalls in the dietary supplement category stem from active degradation caused by improper excipient selection or microbial contamination during raw powder blending. Working with a contract partner operating under 21 CFR Part 111 with in-house HPLC/ICP-MS analytical labs mitigates brand liability significantly.
| Evaluation Pillar | Standard Market Criteria | Tier-1 Enterprise Benchmark (Bactolac Standard) | Strategic Business Impact |
|---|---|---|---|
| cGMP Compliance | Self-certified compliance protocols | Audited 21 CFR Part 111 by NSF, NPA, and FDA registered | Eliminates risk of FDA warning letters and Amazon seller suspensions. |
| Testing Capabilities | Outsourced third-party lab verification | On-site Analytical and Microbiological laboratories | Shortens batch release cycles from 4 weeks to under 7 business days. |
| Delivery Innovation | Standard hard gelatin capsules & compressed tablets | Liposomal powders, chewable bi-layers, gummies, liquid-filled hard veg-caps | Unlocks premium market positioning and consumer compliance differentiation. |
| Supply Chain Traceability | Basic batch records | Full lot quarantine, COA validation, BSE/TSE & Allergen verification | Ensures smooth export customs clearance across EU, GCC, and APAC zones. |
The global multivitamin market is shifting from static, high-dose synthetic blends toward biologically active, targeted matrices. Sourcing managers and brand strategists must anticipate upcoming shifts in consumer demand, ingredient availability, and regulatory frameworks.
Consumers are demanding methylated B-vitamins (5-MTHF L-methylfolate instead of synthetic folic acid, methylcobalamin over cyanocobalamin) and chelated minerals (bisglycinates). Formulators must account for molecular weight differences and density adjustments during blending.
Traditional compressed tablets face consumer pill-fatigue. Sourcing volume is rapidly migrating toward clean-label gummies, single-serve electrolyte powder stick packs, and liquid-filled vegetarian capsules that prevent oxidative degradation of fat-soluble vitamins (A, D3, E, K2).
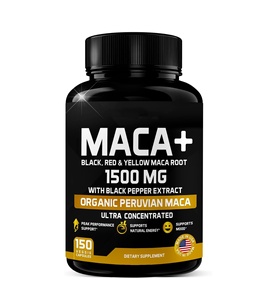
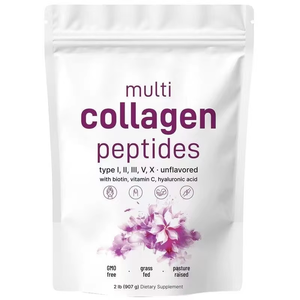
Modern multivitamin procurement prioritizes synergistic formulas combining core daily vitamins with botanical extracts (Maca Root, Ashwagandha), gut health components (spore-forming probiotics), or collagen peptides for dual skin-and-joint benefits.
Developing a stable, high-potency multivitamin requires resolving chemical incompatibilities before commercial scaling. Below are key technical factors evaluated by our formulation scientists during bench-scale trial runs:
Certain vitamins (e.g., Vitamin C, Vitamin B12, and Thiamine) degrade over time when exposed to ambient moisture, heat, or shear friction during compression. A sophisticated supplier calculates precise, safe percentage overages based on real-time and accelerated stability testing, guaranteeing label claim accuracy through expiration.
Hygrscopic powders easily absorb atmospheric moisture, resulting in clumping, uneven capsule fill weights, or tablet capping. Utilizing specialized glidants (e.g., organic rice concentrate, microcrystalline cellulose) ensures high-speed automated encapsulation without compromising clean-label positioning.
Minerals like zinc, copper, and iron, along with B-complex vitamins, carry metallic, bitter taste profiles. Custom powder and drink mix production requires micro-encapsulation techniques and advanced natural flavor-masking systems to create palatability in sachets and chewables.
Operating out of state-of-the-art facilities in Hauppauge, New York, since 1995, our manufacturing partner provides end-to-end solutions for emerging brands, international distributors, and established retail lines.
High-shear, ribbon blending equipment designed for protein isolates, collagen peptides, green superfoods, and electrolyte hydration packets. Flexible automated pouching, stick-pack filling, and wide-mouth jar capabilities.
Get a QuoteEquipped for size 00, 0, and 1 vegetarian (HPMC) and gelatin capsules, liquid-filled hard capsules, and delayed-release options. Complete weight-check control and metal-detection units integrated on every packaging line.
Get a QuoteBi-layer, chewable, sublingual, and enteric-coated tableting engineering. Automated coating pans provide protective moisture barriers, smooth pharmaceutical-grade glazes, or custom natural color finishes.
Get a QuoteEssential answers regarding regulatory documentation, production turnaround times, quality assurances, and custom formulation options.
Connect directly with our technical team to discuss formula feasibility, component lead times, and tier-priced bulk quotes.