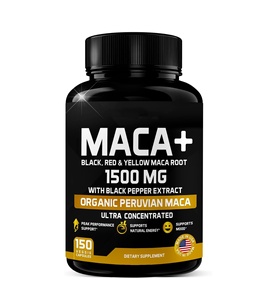
OEM/ODM Private Label 1500mg Maca Root Powder Capsules Red & Yellow Peruvian Botanical Supplement
Standardized Peruvian adaptogenic formulation engineered for bio-energy balance and immune system vitality.
Get Catalog
Explore our wholesale contract-manufactured formulations available for private label customization, bulk order encapsulation, and quick-turnaround OEM distribution.
Standardized Peruvian adaptogenic formulation engineered for bio-energy balance and immune system vitality.
Get Catalog
Multi-strain digestive microflora complex designed specifically to strengthen canine gut-associated lymphoid tissue (GALT).
Get Catalog
Hydrolyzed Type I & III peptides fortified with L-ascorbic acid to stimulate cellular tissue repair and antioxidant defense.
Get Catalog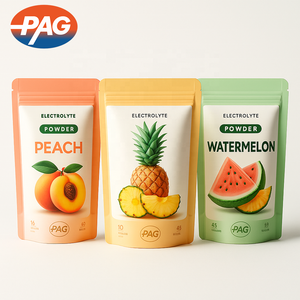
Hypotonic osmolarity blend with trace minerals for rapid cellular rehydration and metabolic homeostasis.
Get Catalog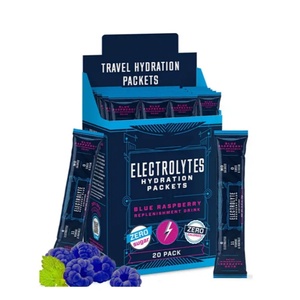
Complete B-complex, Vitamin C, D3, and Zinc premix engineered for instant dissolution and bio-availability.
Get Catalog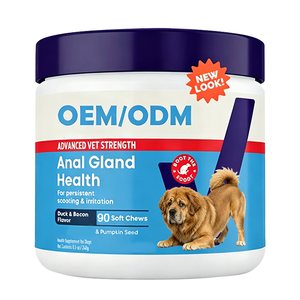
High-fiber botanical soft chews containing pumpkin seed, pectin, and immune-supporting antioxidants.
Get Catalog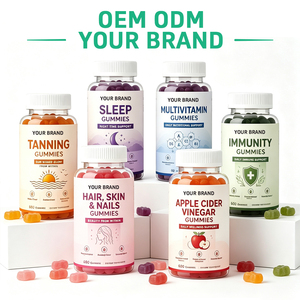
Pectin-based, non-GMO chewable matrix formulated to preserve delicate heat-sensitive immunomodulators.
Get Catalog
Naturally flavored refreshing hydration drink mix formulated without artificial synthetic food dyes.
Get CatalogTechnical Analysis for Procurement Directors, Brand Owners, and Institutional Buyers
The global demand for immunomodulatory and preventative health products has undergone a structural pivot. Modern consumers no longer view immune support as a seasonal intervention; rather, it has transformed into a core pillar of daily baseline wellness. For global brands, selecting the right partner among China wholesale immune support manufacturers and factories requires moving beyond basic unit-cost negotiations to evaluating deep technical capabilities, raw material traceability, analytical precision, and regulatory infrastructure.
China’s nutraceutical contract manufacturing sector has evolved into an advanced technological ecosystem. Combining world-leading fermentation infrastructure, raw botanical extraction capabilities, and automated cleanroom tableting and encapsulation suites, tier-one Chinese factories provide unparalleled production efficiency. However, navigating this landscape requires a sophisticated understanding of ingredient standardization, such as verifying active polysaccharide concentrations in botanical extracts or ensuring the molecular stability of ascorbic acid in complex powdered drink mixes.
Utilizing high-yield submerged fermentation for beta-glucans, cordyceps sinensis, and reishi mycelium to ensure standardized bioactive polysaccharide profiles exceeding 30% purity.
Facilities engineered according to U.S. FDA 21 CFR Part 111 cGMP protocols, ISO 22000, HACCP, and NSF guidelines, backed by comprehensive export documentation packages.
Overcoming bio-absorption barriers through phospholipid bilayer liposomal technology, protecting sensitive vitamins (C, D3, K2) from degradation in gastric environments.
Strategic buyers must anticipate shifting regulatory landscapes, technological advancements, and evolving consumer delivery preferences to maintain market leadership.
While traditional immune products relied heavily on high-dose Vitamin C and Zinc, modern immunobiotic science emphasizes the gut-immune axis. Inactivation of heat-treated postbiotic cells (such as heat-killed Lactobacillus plantarum) allows factory formulators to incorporate immune benefits into liquid preparations, gummies, and baked matrices without loss of viable cell counts over shelf-life.
Global regulatory bodies (notably EU EFSA) have tightened restrictions on traditional binding and flowing agents like titanium dioxide and synthetic magnesium stearate. Advanced Chinese contract manufacturers have modified high-speed tableting lines to utilize organic rice hull concentrates, tapioca maltodextrin, and natural bamboo silica without sacrificing machine throughput.
Consumer demand has shifted away from bulky pill regimens toward functional single-serve stick packs. Modern manufacturing lines feature automated high-precision auger filling capable of dosing micro-encapsulated mineral-vitamin premixes into moisture-barrier laminate sachets at speeds exceeding 300 units per minute.
Future market growth belongs to multi-target functional stacks. Brands are combining immune-defense botanicals (Elderberry, Echinacea, Astragalus) with cellular energy substrates (CoQ10, NAD+ precursors) and adaptogens (Maca, Ashwagandha) to create systemic daily health formulas.
Evaluation of active delivery formats for immune support contract manufacturing.
| Delivery Format | Active Loading Capacity | Bioavailability Index | Moisture Sensitivity | Ideal Immune Actives | Target Shelf Life |
|---|---|---|---|---|---|
| Hard Gelatin/Veggie Capsules | 300mg – 1000mg | Moderate / High | Low – Medium | Herbal extracts, Zinc, Elderberry, Maca, Cordyceps | 24 – 36 Months |
| High-Shear Powders (RTM) | 1000mg – 10,000mg | Rapid Dissolution | High (Requires Sachet) | Collagen Peptides, Electrolytes, Vitamin C, Amino Acids | 24 Months |
| Bi-Layer & Coated Tablets | 500mg – 1500mg | Controlled Release | Low | Multivitamins, Time-Release Ascorbic Acid, Minerals | 36 Months |
| Pectin Soft Gummies | 200mg – 500mg | Gastric Bypass / Oral | High (Temperature Sensitive) | Elderberry Extract, Vitamin D3, Zinc Picolinate | 18 – 24 Months |
Everything that determines whether an immune support formula succeeds on retail shelves—from active ingredient stabilization to analytical lot release—occurs within controlled cleanroom environments under a unified Quality Management System (QMS).
Quality assurance is an engineering requirement, not an afterthought. Raw materials entering the facility are immediately placed into physical quarantine and analyzed using High-Performance Liquid Chromatography (HPLC) for active assay potency and Inductively Coupled Plasma Mass Spectrometry (ICP-MS) for heavy metal trace verification (Lead, Arsenic, Cadmium, Mercury).
Utilizing automated 3D cone blenders and high-shear ribbon mixers, our production lines guarantee homogenicity across micro-dosed active ingredients (such as Selenium or Vitamin D3) down to microgram tolerances, eliminating batch degradation or uneven potency distribution.
Hygroscopic botanicals, effervescent powders, and probiotic blends require strict environmental parameters. Encapsulation and packaging suites operate under Class 100,000 cleanroom standards with active humidity maintained below 35% RH to prevent clumping and premature active degradation.
Whether licensing a proven base formulation or building a custom complex from scratch, our project engineers oversee raw material procurement, pilot batching, label regulatory verification, stability chamber testing under ICH guidelines, and custom packaging finishing (bottles, blister cards, pouches, display boxes).
Detailed technical answers for procurement teams, QA managers, and commercial brand executives.
Maintaining label claim potency requires calculating science-backed manufacturing overages during formulation development. Sensitive vitamins such as L-ascorbic acid or Vitamin D3 naturally degrade over time due to heat, oxygen, and humidity. Responsible manufacturers incorporate targeted overages (typically 5% to 15% above declared label values) based on real-time and accelerated stability testing in environmental chambers (40°C / 75% RH). Furthermore, micro-encapsulation techniques and specialized moisture-barrier packaging (such as aluminum-foil stick packs or amber PET bottles with induction seals) protect sensitive active compounds against oxidative breakdown.
Every commercial production batch should ship with a complete Certificate of Analysis (CoA) verified by internal or accredited third-party laboratories. Crucial documentation includes:
1) Identity Testing: FTIR or HPLC spectrum analysis confirming raw material authenticity;
2) Potency Assays: Quantitative measurement of active markers (e.g., total polyphenols, ginsenosides, zinc elemental content);
3) Microbiological Testing: Total Aerobic Microbial Count (TAMC), Total Yeast/Mold Count (TYMC), and screening for pathogens (E. coli, Salmonella, Staphylococcus aureus);
4) Contaminant Screening: Heavy metals (ICP-MS for Pb, As, Cd, Hg) and pesticide residue screens complying with U.S. USP or European Pharmacopoeia limits. Facilities should hold ISO 22000, HACCP, and 21 CFR Part 111 cGMP compliance audit certificates.
Yes. Leading OEM/ODM manufacturers employ dedicated food scientists and formulation chemists who specialize in custom recipe development. Herbal immune extracts (such as Astragalus, Reishi, or Elderberry) and mineral salts (like Zinc Gluconate) often possess bitter or astringent flavor profiles. In-house R&D teams utilize advanced flavor-masking technologies, natural sweetener systems (Stevia, Erythritol, Monk Fruit), and acidulant balancing (Citric Acid, Malic Acid) to engineer palatable powdered drink mixes, chewable tablets, and functional soft gummies without altering active bio-efficacy.
Production lead times and MOQs depend primarily on raw material availability and the chosen delivery format:
• Stock Formulations / Ready-to-Ship: MOQs typically range from 500 to 1,000 units with dispatch within 7 to 14 days.
• Custom Encapsulation / Tableting: Standard MOQs are usually 100,000 to 300,000 capsules/tablets per batch, requiring 4 to 6 weeks lead time including raw material identity release.
• Custom Powder Drink Mixes & Sachets: MOQs generally start at 30,000 to 50,000 single-serve stick packs, with lead times of 5 to 7 weeks to account for custom foil laminate printing and high-precision pouch filling.
Tier-one manufacturers support international brand owners by providing robust export compliance packages tailored to target regional authorities (such as U.S. FDA, Health Canada, EU EFSA, or Australia TGA). Documentation packages include Certificates of Free Sale (CFS), Health Certificates, BSE/TSE-Free Declarations, Non-GMO Statements, Allergen Statements, and accurate Supplement/Nutrition Facts panels reviewed for proper nomenclature, serving sizes, and claim compliance.
Two-piece hard capsules (gelatin or HPMC hydroxypropyl methylcellulose) and sealed single-serve foil stick pack powders provide the highest level of stability for heat-sensitive botanicals and probiotic strains. Unlike soft gummy manufacturing—which exposes active compounds to high thermal temperatures during starch-molding cooking processes—capsule filling and dry-powder blending occur at ambient temperatures, preserving delicate enzyme structures and volatile phytochemical constituents.
Partner with a verified leader in wholesale contract manufacturing. Connect with our engineering and formulation team to receive custom pricing, batch feasibility studies, and detailed product catalogs.