Explore our pre-formulated, analytical-tested nutraceutical and botanical lines. Every product is manufactured in our Hauppauge, New York facility with full batch tracebility and strict QC release protocols.
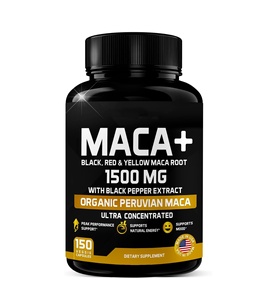
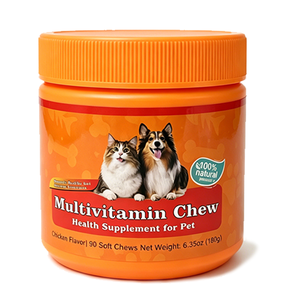
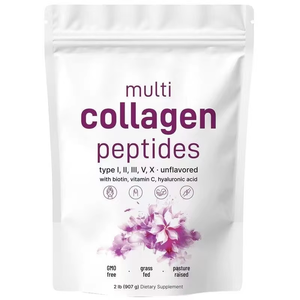
A comprehensive analysis of solid-dose powder processing, batch homogenization, and European Compliance (CE) standardization for global nutraceutical supply chains.
In high-capacity dietary supplement production, dry contract blending is far more complex than simple mechanical agitation. Modern nutraceutical formulations often contain active ingredients with vast disparities in particle bulk density (ranging from 0.2 g/cc to 0.9 g/cc) and particle size distribution (ranging from micro-encapsulated 200-mesh powders to granular 20-mesh botanical extracts). Achieving a target Relative Standard Deviation (RSD) of less than 5.0% across multi-ton production batches requires specialized mixing dynamics, climate-controlled RH (relative humidity) suites, and carefully calculated shear speeds.
“Information Gain Insight: Particle segregation during transport and filling is the primary driver of batch failure in contract manufacturing. Certified facilities utilize geometric dilution protocols and fluid-bed agglomeration to lock micronutrients onto macro-carrier matrices, guaranteeing true label-claim potency per unit.”
At Bactolac Pharmaceutical, our state-of-the-art Hauppauge, NY manufacturing center utilizes high-shear blenders, ribbon blenders, and V-cone blenders fitted with intensifier bars. This multi-suite capability allows our chemical engineering team to tailor blending physics precisely to ingredient vulnerabilities—preventing friction-induced degradation of heat-sensitive vitamins (such as Methylcobalamin B12 and Vitamin C) while ensuring complete dispersion of ultra-low-dose active compounds like Vitamin D3, Chromium Picolinate, and Selenium.
Engineered for complex botanical formulas, superfood greens, and proteins. Our industrial blenders utilize dual-ribbon agitators to create balanced axial and radial flow patterns, eliminating dead spots and preventing agglomeration in hygroscopic herbal extracts.
Every batch undergo rigorous pre- and post-blend testing. Utilizing High-Performance Liquid Chromatography (HPLC) and Inductively Coupled Plasma Mass Spectrometry (ICP-MS), we verify ingredient identity, active potency, heavy metal safety, and microbial clearance before package filling.
From loose powder bulk superfood totes to single-serve stick packs, wide-mouth PET/HDPE jars, gusset pouches, and automated two-piece capsule filling. Fully automated line integration guarantees oxygen barrier protection and shelf-life extension.
Bactolac Pharmaceutical is not merely a contract blender—we are a full-scale pharmaceutical-grade partner committed to quality engineering, regulatory documentation, and brand scale.
Our facility operates strictly under U.S. FDA 21 CFR Part 111 regulations for dietary supplements. Every standard operating procedure (SOP)—from raw material quarantine to finished product release—is documented, audited, and held to pharmaceutical standards. We maintain third-party registrations with NSF, NPA, and QAI Organic certifications.
Supplying markets across the US, EU, UK, Middle East, and Asia-Pacific requires comprehensive regulatory dossiers. Bactolac provides full Certificate of Free Sale, Certificate of Analysis (COA), BSE/TSE-Free declarations, Allergen Statements, and non-GMO documentation tailored to international market clearance.
Select the optimal equipment dynamics based on ingredient physics, target dose precision, and moisture sensitivity.
| Blending Methodology | Ideal Application | Shear Level | RSD Uniformity | Key Quality Benefit |
|---|---|---|---|---|
| High-Shear Agglomeration | Botanicals, Micro-Nutrients, Hydrophobic Actives | High | ✓ < 3.0% | Breaks down oil-rich clumps & coats sub-micron actives evenly. |
| Conical / V-Blender Processing | Fragile Pellets, Probiotics, Vitamin Premixes | Ultra-Low | ✓ < 4.5% | Zero heat generation; preserves live bacterial counts & crystal structures. |
| Double-Ribbon Industrial Mixing | High-Volume Powders, Sports Proteins, Collagen | Medium | ✓ < 4.0% | Rapid bulk throughput with continuous convective particle flow. |
| Fluid-Bed Instantization | Electrolytes, Aminos, Drink Mix Packets | Controlled Steam/Air | ✓ < 2.5% | Lecithin coating for instant cold-water solubility without sinking clumping. |
Insights into the evolving technological and regulatory landscape shaping the global nutraceutical and dietary supplement contract manufacturing sector.
Procurement teams are rapidly transitioning away from legacy synthetic flow agents like Magnesium Stearate, Silicon Dioxide, and Titanium Dioxide. Modern buyers demand clean-label carrier systems using organic rice hulls, bamboo extract silica, and sunflower lecithin. Factories equipped with climate-controlled blending suites can process these natural excipients without suffering line slowdowns or static electricity buildup.
The market for fast-acting functional powders (such as Nootropics, NAD+ precursors like NMN/NR, and Liposomal Vitamin C) requires micro-encapsulation during blending. Coating sensitive molecules in liposomal lipid bilayers protects them through stomach acid passage, dramatically enhancing cellular absorption—a key marketing claim driving premium retail price points.
With global customs tightening regulations on botanical origins and synthetic contaminants, procurement strategies rely on qualified contract manufacturers with established raw material vendor verification programs. Blockchain batch tracking, DNA barcode testing for botanical identity, and complete heavy metal screening (Pb, Cd, As, Hg) have shifted from optional benefits to mandatory procurement requirements.
Consumer preferences have migrated from single-ingredient supplements to multi-functional beverage mixes. Hydration formulas are now expected to include zero-sugar electrolytes, immunity-boosting zinc/vitamin C, and gut-health probiotics simultaneously. Formulating these complex matrices demands expert flavor chemists capable of masking severe bitterness without adding artificial sweeteners.
Detailed answers to key technical, regulatory, and logistics questions from sourcing directors and brand owners.
Scale your supplement brand with pharmaceutical precision, dedicated project management, and turn-key manufacturing from our Hauppauge, New York facility.