Engineered in cGMP (21 CFR Part 111) compliant, CE-certified manufacturing suites with complete analytical release testing and batch traceability.
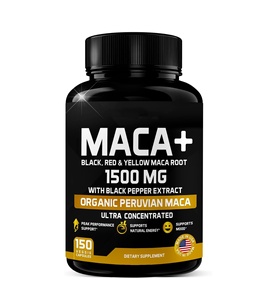
Red & Yellow Peruvian herbal blend with amino acid co-factors for adult endocrine balance, clean energy, and metabolic vitality.
Inquire Now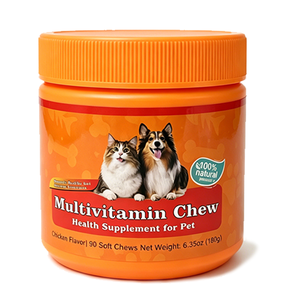
Veterinarian-formulated chewable tablets enriched with essential amino acid profiles and probiotics for balanced canine digestive health.
Inquire Now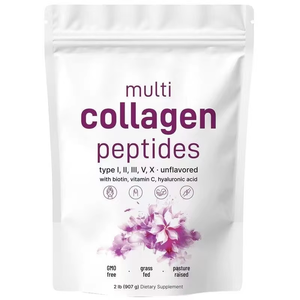
Food-grade bioavailable hydrolysate matrix supporting structural joint integrity, skin elasticity, and collagen synthesis. Keto-friendly.
Inquire Now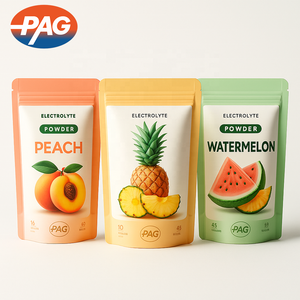
Sports performance intra-workout drink mix featuring instantized BCAAs, key cellular minerals, and zero artificial sugars.
Inquire Now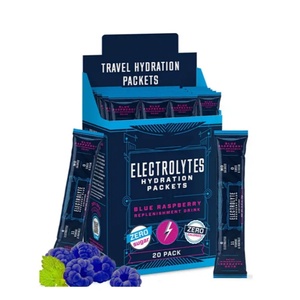
Comprehensive daily electrolyte and micronutrient stick-packs designed for rapid cellular absorption and sustained stamina.
Inquire Now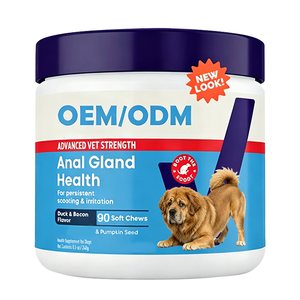
Functional fiber and amino complex targeted for seasonal pet wellness, mucosal lining integrity, and bowel regularisation.
Inquire Now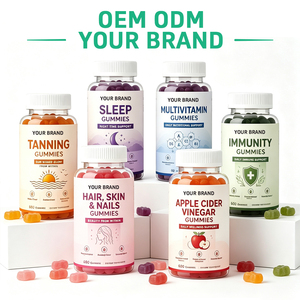
Pectin-based, non-GMO functional vitamin and branched-chain amino acid gummies tailored for brand-specific customer specs.
Inquire Now
Refreshing electrolyte drink mix engineered with balanced osmolarity for quick rehydration across active kids and adult demographics.
Inquire NowThe global demand for high-purity, CE-certified amino acids across pharmaceutical, nutraceutical, and functional food sectors has catalyzed a paradigm shift in industrial bio-manufacturing. As procurement teams evaluate international supply chains, securing amino acids from factories operating under European Conformity (CE) parameters and stringent FDA 21 CFR Part 111 cGMP frameworks is paramount. CE certification—alongside ISO 22000, REACH, and cGMP compliance—serves as an international benchmark verifying that raw raw material synthesis, microbial fermentation, downstream crystallization, and packaging fulfill rigorous safety, environmental, and physical specification thresholds.
Modern amino acid production relies primarily on microbial fermentation (utilizing non-GMO strain lineages of Corynebacterium glutamicum and Escherichia coli) rather than legacy acid hydrolysis of protein biomass. Biological fermentation offers absolute control over enantiomeric specificity, ensuring zero D-amino acid contamination. Downstream processing within our audited facilities incorporates multi-stage continuous crystallizers, ion-exchange chromatography columns, and automated jet-milling suites capable of customizing particle size distributions from 20 mesh granules down to 200 mesh micronized powders.
Utilizing carbon-filtered glucose derived from non-GMO corn starch to guarantee clean substrate metabolism and batch-to-batch consistency.
Advanced lecithin fluid-bed coating techniques transforming hydrophobic BCAAs (Leucine, Isoleucine, Valine) into 100% cold-water soluble powders.
In-house HPLC, LC-MS/MS, and ICP-MS testing verifying chemical assay potency, heavy metal ceilings, microbiological sterility, and residue solvents.
Comparative analytical parameters across industrial amino acid grades produced within CE certified factory networks.
| Amino Acid Grade | Assay Purity (HPLC) | Heavy Metals (ICP-MS) | Endotoxin Limit | CE & Regulatory Compliance | Primary Industrial Applications |
|---|---|---|---|---|---|
| Pharma Injectable Grade | ≥ 99.5% - 100.5% | < 1 ppm Lead/Arsenic | < 0.25 EU/mg | CE Certified / EP / USP | Medical Nutrition, Infusions, API Precursors |
| Nutraceutical Fermentation Grade | ≥ 98.5% - 100.0% | < 3 ppm Total Heavy Metals | Non-Pyrogenic Verified | CE Certified / 21 CFR 111 | Sports Dietary Supplements, BCAAs/EAAs, Gummies |
| Instantized Food & Beverage Grade | ≥ 98.0% - 99.5% | < 5 ppm Total Heavy Metals | Food Safety Compliant | CE Certified / ISO 22000 | Electrolyte Drink Powders, Functional Foods |
| Veterinary & Pet Health Grade | ≥ 97.0% - 99.0% | < 10 ppm Total Heavy Metals | Feed Grade Standard | CE Certified / FAMI-QS | Canine Joint & Digestive Formulas, Pet Supplements |
As global supply chains navigate regulatory tightening and heightened consumer demand for clean-label credentials, procurement officers must align with factories capable of integrating next-generation bio-manufacturing trends. The next decade of amino acid manufacturing is defined by three pivotal structural shifts:
Transitioning from traditional crop-derived starch substrates toward engineered micro-algal and synthetic bacterial chassis. This increases volumetric fermentation yields by up to 35% while slashing water consumption and land usage footprints, ensuring long-term price stability for enterprise buyers.
EU regulatory frameworks (including CBAM and updated CE environmental directives) increasingly penalize carbon-intensive chemical synthesis. Forward-thinking factories are adopting solar-powered bioreactors and closed-loop water recycle loops to deliver verified net-zero amino acid raw materials.
Consumer preference for RTD (Ready-To-Drink) beverages and clear protein waters has driven demand for allergen-free instantization. Sunflower-lecithin coating and nano-encapsulation technologies eliminate bitter off-notes and prevent floating residue without compromising biological activity.
With over 30 years of specialized experience in nutraceutical and amino acid processing, our turn-key infrastructure bridges raw material fermentation with finished, market-ready consumer products. By centralizing formulation science, blending, encapsulation, tableting, laboratory verification, and full packaging under a unified quality management system, we eliminate supply chain friction and regulatory risk.
Dedicated technical project managers oversee your master batch records (MBR), raw material qualification, analytical COAs, and shipping logistics from day one.
Analytical chemistry labs equipped with HPLC, UV-Vis, FTIR, and microbiological testing guarantee every batch meets rigid identity, strength, and purity specifications.
From 25kg fiber drums for bulk B2B raw powder distribution to high-speed stick-packing, jar filling, blister packaging, and custom labeling for DTC brands.
A CE certified amino acid manufacturing facility strictly adheres to European Union health, safety, and environmental protection requirements. For amino acids used in medical foods, pharmaceuticals, or functional health products, CE alignment verifies that equipment design, cleanroom air quality (ISO Class 7/8), water purification (USP Purified Water/WFI), continuous risk analysis (HACCP), and trace-level chemical residue limits comply with European Directive standards.
Enantiomeric purity is verified in our on-site laboratories using High-Performance Liquid Chromatography (HPLC) fitted with chiral stationary phase columns and polarimetric optical rotation analysis. This ensures that synthesized or fermented amino acids (such as L-Leucine, L-Glutamine, or L-Theanine) maintain greater than 99.5% L-form enantiomeric excess, preventing bio-inactive or undesirable D-form isomers from entering the finished batch.
For standard bulk raw materials, MOQs start at 25kg (1 standard drum). For custom contract manufacturing including high-shear powder blending, capsule encapsulation, or custom tableting, MOQs typically begin at 1,000 units for finished bottled products or 100,000 capsules/tablets per batch run, allowing emerging and established brands to scale efficiently.
Yes. Every production run is issued a full Certificate of Analysis (COA) detailing physical, chemical, and microbiological specifications. Additionally, we provide Certificate of Free Sale (CFS), BSE/TSE-Free Declarations, Allergen Statements, Non-GMO Verification, and Halal/Kosher documentation upon request to facilitate seamless customs clearance across European, North American, Asian, and Middle Eastern entry points.
Hydrophobic amino acids (Leucine, Isoleucine, Valine) naturally resist water dissolution. We utilize advanced fluid-bed micro-encapsulation techniques using sunflower lecithin or non-GMO soy lecithin. This creates a thin hydrophilic coating on each particle crystal, lowering surface tension and allowing the powder to dissolve completely in cold water within 30 seconds without foaming or clumping.
Standard production turnaround for repeat orders ranges from 3 to 4 weeks. For new custom formulations requiring benchtop pilot sampling, flavor profiling, stability testing, and custom packaging component procurement, the initial project cycle typically spans 6 to 8 weeks. Expedited production schedules are available upon technical review.
Initiate your custom formulation project, request enterprise volume quotes, or consult with our senior formulation scientists today.