Selecting the best China supplier for Bi-Layer Tablets requires more than comparing prices or factory photographs. The dosage form combines two formulation layers, often with different release profiles, compression forces, and excipient requirements. Small variations can affect layer bonding, weight uniformity, dissolution, and long-term stability. Manufacturing experience matters.
The IQVIA Institute’s Global Use of Medicines 2024 report projects continued growth in global medicine spending through 2028. This trend increases demand for efficient, scalable, and quality-controlled oral solid dosage manufacturing. Grand View Research also identifies pharmaceutical contract manufacturing as a growing sector, supported by outsourcing and capacity expansion. These reports suggest opportunity, but market growth alone does not prove supplier capability.
A reliable Chinese manufacturer should provide GMP evidence, process validation records, stability data, and transparent batch documentation. Review the tablet press model, maximum compression force, layer-weight control, and in-process testing. Ask how operators manage powder segregation, sticking, capping, and dissolution differences between layers. Request representative samples, not only catalog images. The FDA’s process validation guidance supports a lifecycle approach, covering process design, qualification, and continued verification.
No supplier is perfect. A polished brochure is not evidence. Buyers should independently verify certifications, audit production areas, and assess technical communication before signing a contract. The best partner is not always the largest factory. It is the supplier that can repeatedly produce consistent Bi-Layer Tablets, explain deviations clearly, and support regulatory documentation across development and commercial stages.
China Best Bi-Layer Tablets Manufacturer Supplier?
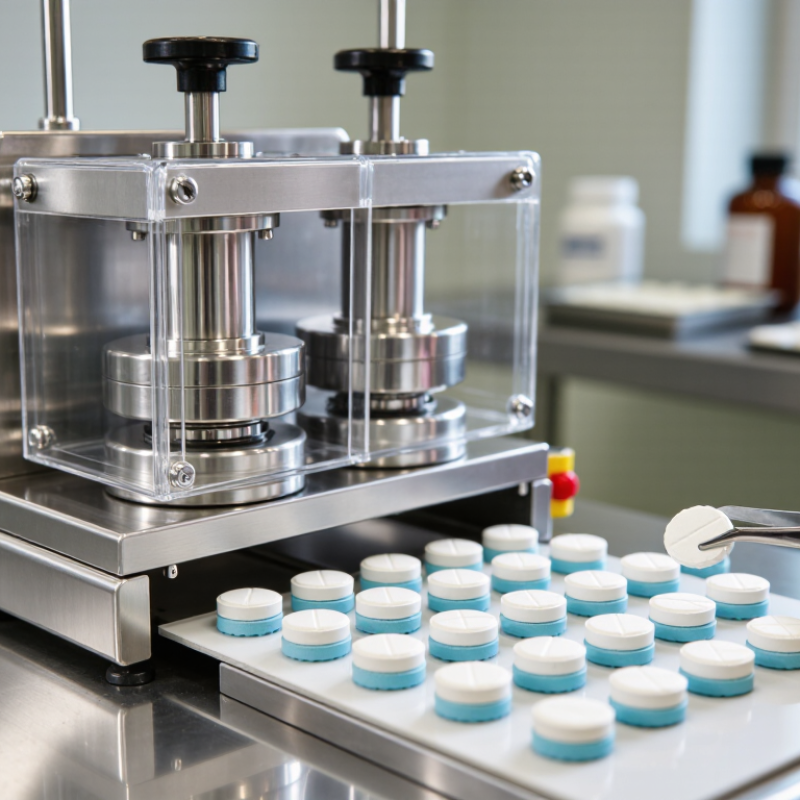
Bi-layer tablets combine two separate layers in one solid dosage form. Each layer can contain a different active pharmaceutical ingredient, or API. This design helps manage incompatible ingredients, different release rates, or separate dosing needs. One layer may release quickly, while the second works gradually. The tablet looks simple. The formulation work is not.
Experienced manufacturers control powder flow, layer weight, compression force, and tablet hardness. They also test separation, friability, dissolution, assay, and stability. A reliable supplier should provide development records, batch traceability, validated testing methods, and clear production controls. Engineers must examine API compatibility before selecting excipients. Poor bonding can cause cracks or layer separation during packaging. That detail is easy to underestimate.
Tips: Ask for pilot-batch data, not only finished samples. Review dissolution results for both layers. Confirm how cross-contamination is prevented between manufacturing stages. Check whether the supplier can adjust layer thickness without disturbing dose accuracy. It is also wise to discuss packaging early, because moisture can affect tablet strength. A polished sample proves little. Real consistency matters more. One concern remains: laboratory performance may change during scale-up. Careful process review is still necessary.
A bi-layer tablet combines two separately compressed layers in one dosage unit. Each layer can contain a different active pharmaceutical ingredient (API), allowing controlled separation, independent formulation, or different release characteristics within the same tablet.
China Best Bi-Layer Tablets Manufacturer Supplier?
For bi-layer tablets, quality begins with layer control, not appearance. USP–NF General Chapter <905> sets an Acceptance Value of no more than 15.0 for dosage-unit uniformity. The calculation considers the average result and dosage-unit variability. Each active layer needs separate evaluation when strengths or release profiles differ. A tablet can look perfect and still fail testing.
Manufacturers should sample both layers during compression. Weight checks, assay testing, and blend uniformity data help locate segregation or layer contamination. FDA Process Validation guidance recommends linking process performance with measurable quality attributes. In practice, compression speed, feeder vibration, and transfer pressure can shift the result. Small changes matter.
Tips: Request recent <905> test records, layer-specific assay data, and deviation histories. Check whether the supplier reports AV values, not only average potency. Confirm method validation, analyst training, and stability results. USP <905> is a benchmark, not a guarantee. Some specifications still need product-specific justification. A weakness remains common: suppliers may test the finished tablet but overlook sampling bias during production. Ask how samples were collected, stored, and retested.
An anonymized quality-benchmark framework for evaluating bi-layer tablet manufacturing capability. Product-specific specifications and validated test methods remain applicable.
| Quality Dimension | Test or Control Point | Benchmark / Acceptance Requirement | Illustrative Data Set | Assessment | Reference / Technical Note |
|---|---|---|---|---|---|
| Dosage-unit uniformity | USP <905> Acceptance Value (AV) | AV ≤ 15.0 at the applicable stage of testing. | AV = 8.7 for the initial 10-unit sample | Pass | USP <905> Uniformity of Dosage Units. The calculation uses the individual dosage-unit results, the reference value M, and the variability term. |
| Dosage-unit uniformity | Individual content or mass results | For the standard Level 1 assessment, individual results should remain within the applicable USP <905> limits; the AV criterion must also be met. | 10 units: 96%, 98%, 99%, 101%, 97%, 100%, 102%, 98%, 99%, 100% | Pass | The exact calculation and permitted ranges depend on the dosage form, assay basis, and monograph requirements. |
| Content uniformity | Assay of the active ingredient in each layer | Use the approved product specification and a validated analytical method; the specification must be consistent with the applicable pharmacopoeial requirement. | Layer A: 98.6% of label claim Layer B: 99.3% of label claim |
Within target | A bi-layer tablet requires separate consideration of each active ingredient and potential cross-layer sampling effects. |
| Layer weight control | Individual layer weight and total tablet weight | Controlled against the approved batch specification and validated process capability; limits are product-specific rather than universally fixed by USP. | Target total weight: 650 mg Average measured weight: 648.4 mg Relative deviation: −0.25% |
Within target | In-process controls commonly include feeder performance, compression force, fill depth, and periodic weight checks for both layers. |
| Layer ratio | Mass ratio between Layer A and Layer B | Must remain within the validated product-specific operating range to support dose accuracy and dissolution performance. | Target ratio: 60:40 Measured average ratio: 59.6:40.4 |
Within target | Layer ratio limits should be justified by development studies, risk assessment, and process validation data. |
| Mechanical strength | Tablet hardness or breaking force | Must be strong enough for handling and packaging while remaining suitable for disintegration and dissolution. | Average breaking force: 105 N Range: 96–114 N |
Within target | There is no single universal hardness limit for all tablets; the approved product specification controls acceptance. |
| Friability | Mass loss after friability testing | Common compendial benchmark: not more than 1.0% mass loss unless otherwise specified. | Mass loss: 0.32% | Pass | The applicable pharmacopoeial procedure and product monograph should be confirmed before release testing. |
| Disintegration | Disintegration time of the complete bi-layer tablet | Must comply with the approved product specification and applicable dosage-form monograph. | Average time: 7 minutes 42 seconds Maximum observed time: 8 minutes 31 seconds |
Within target | The limit depends on the dosage form, release design, formulation, and relevant pharmacopoeial requirements. |
| Dissolution performance | Stage-specific dissolution profile for each active ingredient | Must meet the approved Q value, time point, apparatus, medium, and sampling requirements. | Active A: 93% released at the specified time point Active B: 91% released at the specified time point |
Meets example target | Dissolution acceptance criteria are product-specific; USP does not assign one universal numerical limit to all bi-layer tablets. |
| Layer interface integrity | Visual and mechanical inspection of the boundary between layers | No visible separation, capping, lamination, cracks, or unacceptable mixing at the interface. | Inspected units: 30 Defects observed: 0 |
Pass | Interface integrity should be verified during compression, coating if applicable, accelerated stability, and transport simulation. |
| Appearance and dimensions | Color, shape, debossing, diameter, and thickness | Must conform to approved artwork, tooling, and dimensional specifications. | Diameter: 11.02 mm average Thickness: 5.84 mm average Visual defects: none observed |
Conforms | Dimensional limits are established during product development and tooling qualification. |
| Moisture control | Loss on drying or water content | Must remain within the formulation-specific range established for flowability, compression, stability, and layer adhesion. | Water content: 1.8% w/w Validated operating range: 1.0–2.5% w/w |
Within range | Moisture limits should be supported by stability and process-development data. |
| Batch traceability | Documentation and record review | Complete batch manufacturing records, laboratory records, equipment logs, deviation records, and release authorization must be available. | Records reviewed: 12 of 12 required categories Unresolved critical deviations: 0 |
Complete | Quality-system documentation is essential when assessing a contract manufacturer or supplier. |
Note: The numerical results shown as an illustrative, anonymized evaluation dataset are not attributed to any company or brand. Final release decisions must use the approved product specification, validated analytical methods, applicable pharmacopoeial requirements, and authorized quality records.
A qualified bi-layer tablet supplier must control each layer, not only the finished tablet. Under cGMP Parts 210–211, procedures should protect identity, strength, quality, and purity. Operators should record material status, room conditions, equipment cleaning, and batch decisions in real time. Paperwork cannot repair weak process control.
Layer separation is a practical risk. Uneven die filling, excessive compression force, or poor transfer timing can create visible cracks. In-process checks should monitor tablet weight, hardness, thickness, friability, disintegration, and layer adhesion. Sampling plans need scientific justification. “Looks acceptable” is not enough.
The FDA’s 2019 Drug Shortages Task Force report found that manufacturing and product-quality problems contributed to 62% of shortages reviewed from 2013 to 2017. That figure shows why supplier qualification deserves more than a questionnaire. Audit evidence should include process validation, cleaning validation, deviation investigations, change control, stability data, and laboratory records. Suppliers should also demonstrate traceable calibration and controlled electronic data.
Small gaps matter.
A weak investigation may hide recurring failures. A perfect-looking batch can still reflect an unstable process. Buyers should compare actual control charts, not only certificates. The FDA’s guidance on process validation supports continued process verification, yet some supplier reviews still stop after initial qualification. That is an area worth challenging.
China Best Bi-Layer Tablets Manufacturer Supplier?
Choosing a bi-layer tablet supplier requires more than checking annual output. Press capacity should match the product’s actual needs. Review turret speed, feeder design, compression force, and changeover time. A large press may still perform poorly with delicate formulations.
Ask for production records from comparable tablet sizes. During a technical audit, observe first-layer thickness, transfer stability, and second-layer compression. Layer weight control deserves close attention. Suppliers should use calibrated feeders, in-process weighing, and documented sampling plans. Small weight shifts can affect dose uniformity, hardness, and dissolution. Data matters most.
Request OOS rates for the previous twelve months, separated by cause. Useful categories include weight variation, hardness, sticking, layer separation, and assay results. Do not accept one impressive percentage without definitions. Review deviation investigations and corrective actions. A low OOS rate may reflect strong control, but it may also reflect weak reporting. That deserves scrutiny.
Practical trials reveal more than polished presentations. Compare pilot results with routine batch records. Check whether operators react consistently when humidity or powder flow changes. Ask how rejected tablets are handled and reconciled. Some suppliers provide excellent samples but struggle during scale-up. I have seen this gap become expensive. A transparent supplier will admit process limits, share trend data, and explain what still needs improvement.
Selecting a bi-layer tablet supplier requires more than comparing prices. A practical audit should inspect granulation rooms, compression lines, cleaning records, and humidity controls. Ask for batch records, deviation logs, and recent product-quality reviews. The WHO Good Manufacturing Practices framework stresses documented controls, traceability, and validated processes. A certificate alone is not proof.
Validation deserves close attention. Request process-validation protocols covering layer weight, hardness, dissolution, and cross-contamination risks. ICH Q8, Q9, and Q10 provide useful references for pharmaceutical development, risk management, and quality systems. Check whether analytical methods are validated under ICH Q2 principles. Review three consecutive commercial batches when possible. Small details matter, such as separate sampling tools and visible line-clearance checks. A polished file can still hide weak shop-floor habits.
Certifications should match the destination market and dosage form. Verify certificate numbers directly through the issuing authority, then compare them with audit findings. Export history also needs evidence. Use China Customs records and UN Comtrade HS 3004 data to examine shipment consistency, destination markets, and unusual volume changes. Export data is helpful, but incomplete. It may not show rejected batches or private-label relationships. Ask for redacted shipping documents, inspection reports, and stability data. I would score technical transparency above a low quotation. That judgment is imperfect, but safer.
It is one tablet made from two separate compressed layers. Each layer may contain a different active ingredient or release pattern.
Two layers can separate incompatible ingredients. One layer may release quickly, while the other releases gradually.
Manufacturers should control powder flow, layer weight, compression force, hardness, and transfer timing. Small changes can affect dose accuracy.
Engineers should optimize powder properties and compression settings. They should inspect cracks, adhesion, friability, and tablet strength during production.
Request dissolution results for both layers, assay data, stability results, and uniformity testing. Pilot-batch records are more useful than attractive samples.
Review press speed, feeder design, compression range, and changeover time. A large machine may still perform poorly with sensitive powders.
Review batch traceability, cleaning records, calibration data, deviation investigations, and change-control documents. Certificates alone prove little.
Ask for twelve months of results, separated by cause. Low reported failures may indicate strong control, but incomplete reporting is also possible.
Not always. Humidity, powder flow, and transfer timing may change during scale-up, so continued process review remains necessary.
Bi-Layer Tablets provide a practical dosage form for combining two active pharmaceutical ingredients or separating incompatible materials within one tablet. By placing each formulation in a distinct layer, manufacturers can support controlled dosing, improve product stability, and simplify administration. Reliable production requires precise control of layer weight, compression force, hardness, dissolution, and tablet-to-tablet consistency. Quality testing should include USP <905> uniformity assessment, with the acceptance value maintained at or below 15.0 where applicable.
When selecting a China-based tablet supplier, buyers should evaluate production capacity, equipment suitability, cGMP compliance under 21 CFR Parts 210–211, process validation, cleaning controls, and documented out-of-specification rates. Supplier audits should also review quality systems, laboratory practices, certifications, export experience, and batch traceability. A qualified manufacturer should provide transparent technical documentation, stable capacity for commercial production, and effective controls that protect product quality from development through shipment.